Protecting Brand Integrity with GMI-Certified Color Control
Color on packaging is a critical technical asset. It enables rapid product recognition at the shelf, clear differentiation of strengths and warnings for regulators, and reliable compliance with retailer packaging specifications. When color varies from run to run or plant to plant, that variation introduces operational and brand risk in the form of delays, rework, rejected lots, and lost shelf space during high-pressure resets and seasonal programs.
GMI (Graphic Measures International) establishes rigorous third-party standards for color control, print process stability, and documentation in packaging print. Many national retailers and global brands now mandate GMI-certified label printing to ensure that approved colors reproduce consistently across substrates, plants, presses, and regions. For packaging, quality, and procurement teams, GMI Certification transforms color from subjective opinion into audited, data-driven performance and significantly reduces brand risk.
At DG Labels, we are a GMI-certified, high-precision label manufacturer. We provide:
- GMI-certified flexographic, digital, and offset printing platforms
- Comprehensive color management and spectral color control
- Full bindery and finishing services
- Integrated direct mail formats aligned with on-pack branding
This article outlines how to establish and maintain a brand-safe, GMI-compliant color library using defined color targets, controlled proofs, ink drawdowns, and realistic tolerances so every production run supports global color accuracy and minimizes brand risk.
Why a Brand-Safe, GMI-Controlled Color Library Is a Strategic Asset
A brand-safe color library is a controlled system of color standards that is both technically defined and operationally enforced. A robust library is:
- Defined with numeric color data (e.g., spectral and Lab values) for every key hue
- Documented across substrates and print methods
- Measured and verified in production, not just evaluated on-screen
- Shared across design, prepress, pressroom, and quality teams
Without this structure, color decisions drift and introduce risk. Unmanaged color can result in:
- Packaging that fails retail packaging approval and color compliance checks
- Heightened regulatory scrutiny in categories such as OTC, nutraceuticals, or food
- Consumer confusion when line extensions do not appear visually related
- Costly reprints, relabeling, or repackaging when batches fall outside specification
GMI-certified label printing imposes disciplined process control on this environment. Instead of subjective judgments, color is approved against documented targets and tolerances that are audited and monitored. This consistency becomes even more critical as brands scale across languages, regions, multiple packaging formats, and seasonal SKUs that all must present as one unified, trusted brand.
For CPG, healthcare, and industrial brands, a centralized, GMI-driven color library supports:
- Core brand colors applied consistently across all SKUs and formats
- Limited-time offers and seasonal designs that still match the parent line
- Multi-plant and multi-technology production with aligned, measurable expectations
When your color library is well defined, centrally controlled, and accessible, every new label starts from approved, measurable color standards instead of introducing new, unmanaged color variables.
Establishing GMI-Compliant Color Targets and Standards
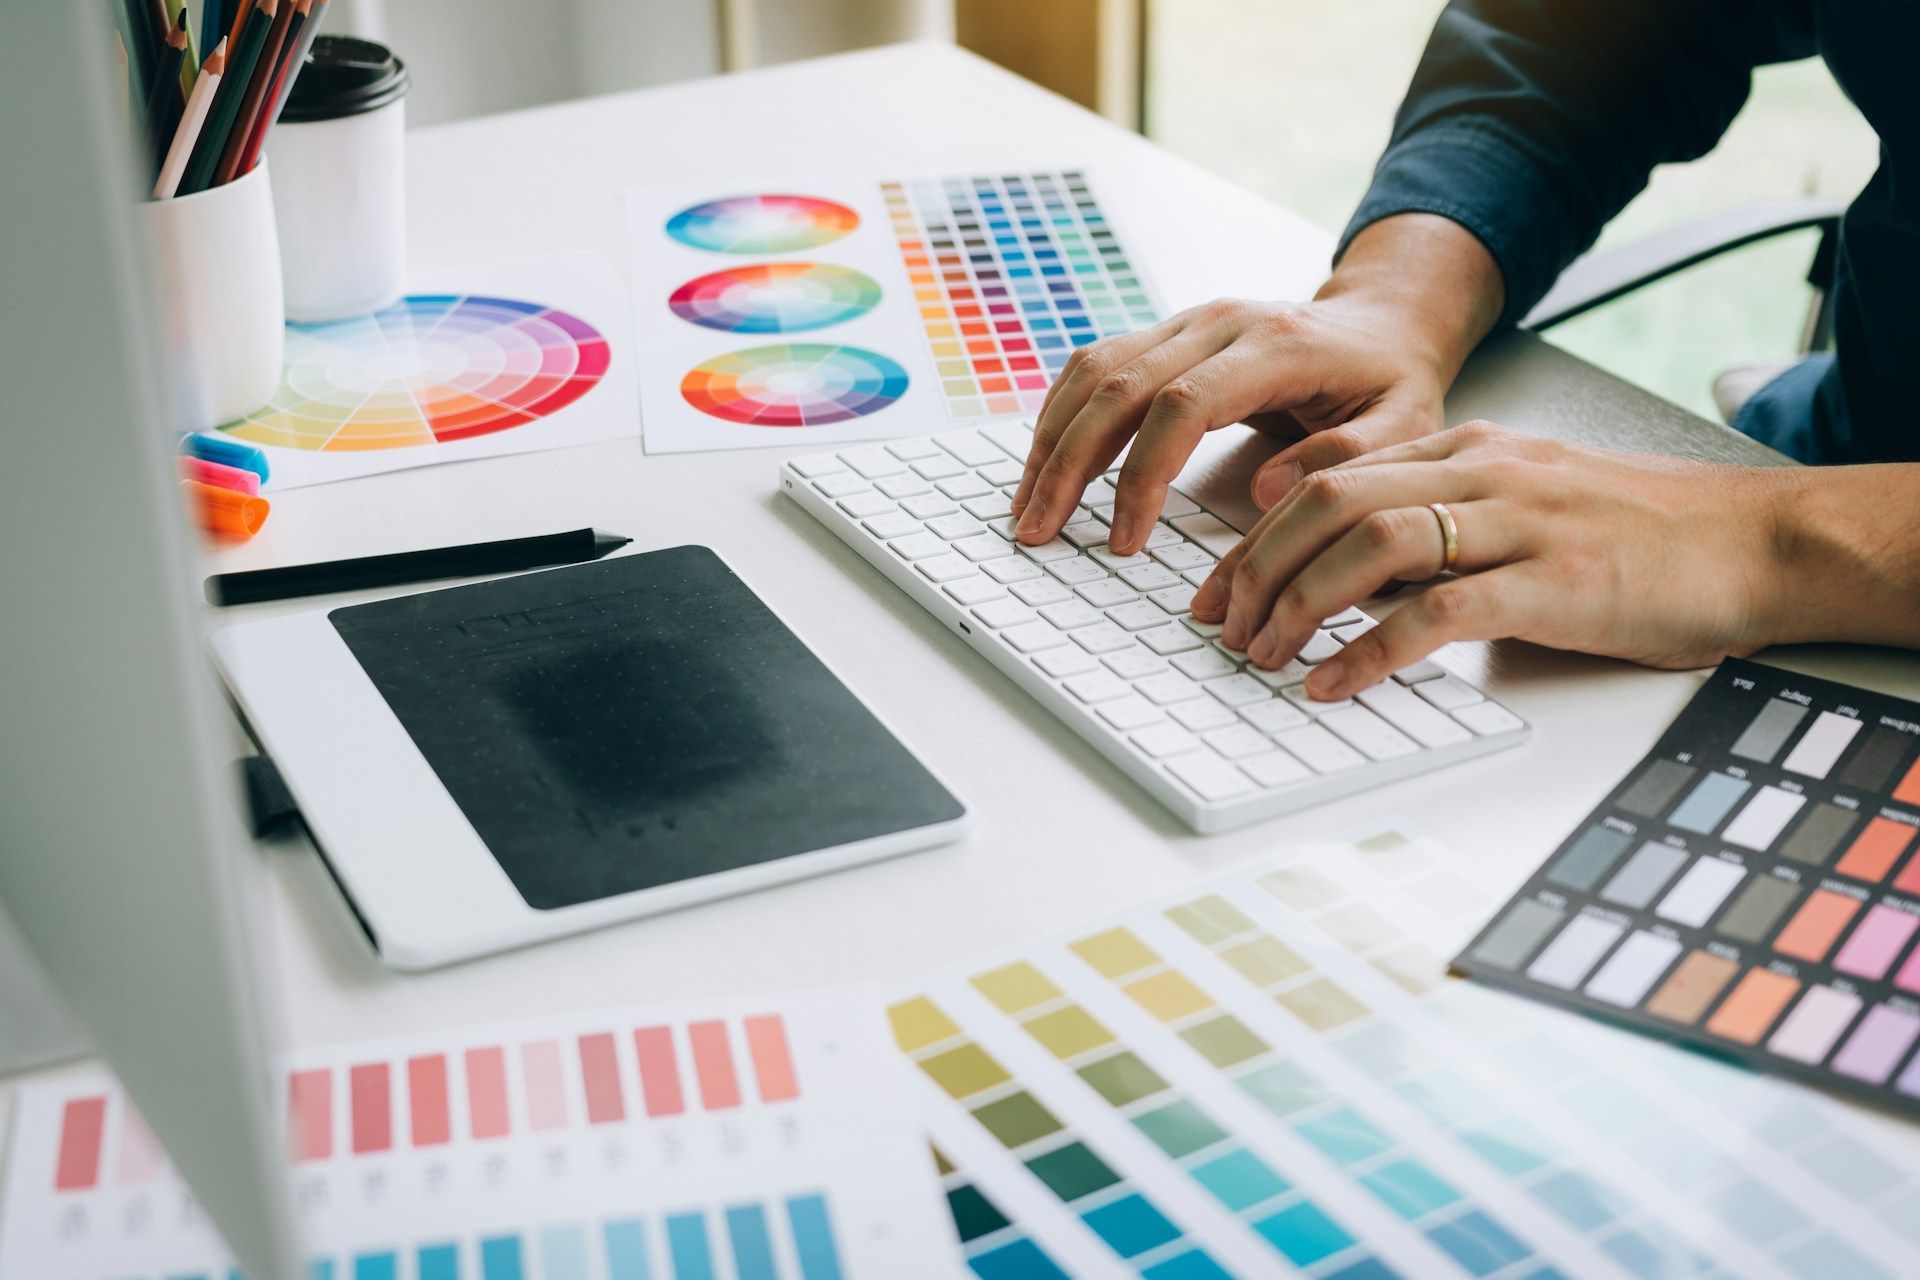
Color targets are the foundation of a controlled color library. These master references describe each brand color using precise spectral data rather than relying on approximate names or visual swatches.
A robust color target typically includes:
- Lab values and full colorimetric data
- Ink density and trapping guidelines where applicable
- Defined tolerances for acceptable variation, such as ΔE limits
- Documentation by substrate and print process
At DG Labels, we create and validate these targets within GMI-approved workflows specifically engineered for global color accuracy and brand risk reduction. Our proofing systems are calibrated to our production presses, and we measure color with spectrophotometers to confirm that targets are both realistic and repeatable on flexographic, digital, and offset platforms.
Substrate definition is critical. The same ink formulation will not present identically on different materials, such as:
- Paper vs. film vs. foil
- Coated vs. uncoated stocks
- White vs. clear or metallic bases
Whiteness, opacity, coating, and absorption all influence the final appearance. Accordingly, we establish related, substrate-specific targets for each major material category. We then align flexographic, digital, and offset targets to be perceptually consistent while honoring the color gamut limitations of each process.
These targets reside in a controlled digital color library with:
- Version history and revision tracking
- Defined ownership, signoff, and approval records
- Alignment with GMI documentation, reporting, and audit requirements
When your team updates artwork or launches a new SKU, they work from these approved, auditable standards rather than unintentionally creating new colors that increase brand risk.
Using Proofs and Ink Drawdowns for Predictable, GMI-Certified Outcomes
Color targets define the objective; proofs and ink drawdowns verify that production can meet that objective before full-scale manufacturing. This step is integral to maintaining GMI-certified performance and avoiding downstream risk.
Three key tools support this process:
- Digital contract proofs: Color-calibrated proofs that simulate the final label and serve as formal approval documents.
- Press proofs: Short runs on the production press, on the final substrate, under actual production conditions.
- Ink drawdowns: Controlled applications of ink directly on the specified substrate to evaluate hue, opacity, and dryback behavior.
At DG Labels, we generate contract proofs tightly matched to press conditions so they are both visually and numerically aligned with your targets and with GMI requirements. Brand and quality teams can approve based on measured data and visual correlation, ensuring that print outcomes support defined specifications.
Ink drawdowns provide additional assurance by illustrating how an ink behaves on the actual substrate. They help answer technical questions such as:
- Is color strength sufficient on this film, paper, or foil substrate?
- Does the shade shift as the ink dries and cures?
- How does the ink trap over or under other colors in the design?
We measure proofs and drawdowns with spectrophotometers and compare results directly to your master targets. This closes the loop from design intent to ink formulation to press performance. Within a GMI-certified framework, this process substantially reduces the likelihood of rework, rejected lots, or late-stage color disputes.
Setting Practical Color Tolerances for Global Consistency
Even with precise control, production cannot achieve a zero-variation outcome. Clearly defined, realistic tolerances are essential for global consistency and for satisfying GMI requirements.
Color tolerances define the acceptable deviation from the target at which color is still considered on-spec. These tolerances typically include:
- ΔE thresholds for spot and critical process colors
- Density ranges for process builds
- Gray balance and tonal value increase (TVI) targets
At DG Labels, we collaborate with brand owners to set tolerances that are stringent enough to protect brand equity and retailer expectations, yet achievable across flexographic, digital, and offset technologies on different substrates. These tolerances are documented and integrated into our GMI-certified quality control procedures.
Two additional factors are important:
- Viewing conditions: Labels can appear different in a controlled light booth than in a retail environment. We combine instrumental data with controlled visual checks under standardized lighting so that decisions align with real-world appearance.
- Data logging and reporting: Ongoing measurements, color bar checks, and GMI performance tracking maintain production within tolerance over time, not just on initial runs.
This disciplined approach significantly reduces the risk of rejected shipments, retailer chargebacks, or urgent relabeling when volumes peak and distribution expands.
Maintaining Color Integrity Across Substrates, Finishing, and Channels
Color accuracy is influenced not only by ink and substrate but also by finishing processes. Coatings, laminations, foils, and varnishes alter gloss, contrast, and depth, all of which affect how the same ink is perceived.
A comprehensive, GMI-aligned color library should define:
- Target finishes for each SKU, such as matte varnish, gloss varnish, or gloss laminate
- Any special effects, such as metallics or foils, that interact with color
- Visual alignment requirements between primary labels, cartons, and mailers
At DG Labels, we manage color through the entire converting and finishing workflow, including full bindery and direct mail formats. Our GMI-certified processes ensure that on-shelf packaging aligns visually with related components that arrive via mail or other channels, reinforcing a unified brand presentation.
For brands managing families of SKUs and complex line architectures, we emphasize:
- Shared core colors across strength, dosage, or flavor variants
- Consistent handling of regulatory and compliance elements that can influence color perception
- Standardization across all items that share a shelf, ship together, or appear within a coordinated campaign
Through regular calibration, process control charts, and ongoing GMI audits, once your color specifications are defined, they remain stable from run to run and from season to season, supporting both operational reliability and brand protection.
Turn Your GMI-Certified Color Program Into a Competitive Advantage
A disciplined, GMI-certified color management program transforms your color library into a strategic business asset. Clearly defined targets, controlled proofing and ink drawdowns, and practical tolerances reduce brand and supply chain risk, protect shelf impact, and build trust with retailers that rely on repeatable, documented performance.
At DG Labels, we support this full workflow with:
- GMI-certified label printing across flexographic, digital, and offset platforms
- Advanced color management and spectral measurement for global color accuracy
- Comprehensive finishing, bindery, and direct mail capabilities aligned with regulated and brand-driven markets
With a structured, GMI-driven color library in place, every new label, extension, or campaign can move efficiently from approval to shelf with a high degree of confidence in how your brand will present when it matters most.
Request a Quote
To apply GMI-certified color control to your next packaging or label program and reduce brand risk across your global supply chain, request a quote from DG Labels today. Our team will review your specifications, substrates, and regulatory requirements to design a color management and production plan that supports precise, repeatable performance.
Get Started With Your Project Today
If you are ready to improve print consistency and color accuracy across every run, our
GMI-certified label printing process is built to meet strict brand standards. At DG Labels, we collaborate with your team to match your exact specifications and keep your labels performing on shelf. Share a few details about your project and we will recommend the best materials, finishes, and print approach. To request a quote or discuss timelines, simply
contact us.